As a MJP 3D printer supplier, I get this question every single day: “What’s the build volume of your machines?” It makes sense—build volume is one of the first specs anyone looks at when shopping for a 3D printer, right? Too small, and you can’t print the part you need. Too big, and you’re wasting material and money on unused space. But if you think MJP (Multi-Jet Printing) build volume is just a single number, you’re missing half the story. Let me break this down, not as a sales pitch, but as someone who’s spent the last 8 years troubleshooting, testing, and fine-tuning these printers for manufacturers, prototypers, and even small businesses that walk into my workshop. MJP 3D Printer
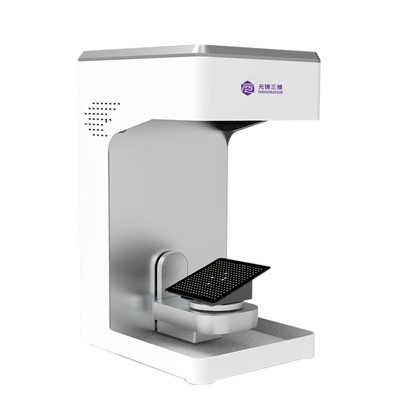
First, let’s start with the basics: what even is MJP build volume, versus other 3D printing technologies? FDM (Fused Deposition Modeling) printers usually list build volume as a single cube, like 300x300x400mm, and that’s mostly consistent—you measure the maximum space the nozzle can move, minus a tiny safety buffer for the build plate bed. SLA (Stereolithography) is a little different, but still, it’s the maximum area the laser can scan. MJP? It’s a hybrid. MJP uses thousands of tiny nozzles to jet wax support material and photopolymer build material layer by layer. Those nozzles are mounted on a gantry, but the way the material is jetted, cured, and removed adds little hidden layers that affect the usable space. I once had a customer who ordered a machine expecting a 400mm x 400mm bed, and got a surprise when his 380mm long car door hinge arm wouldn’t fit. He’d forgotten that the MJP process requires a small gap at the edges for the wiper blades that smooth each layer. That’s the key mistake people make: build volume for MJP isn’t just the gantry’s total movement—it’s the usable, printable volume.
Now, for our line of MJP printers, let’s get specific. Our entry-level machine, designed for small prototyping shops, has a usable build volume of 350mm (length) x 350mm (width) x 400mm (height). Wait, why not round it to 350x350x400mm? Because that’s the actual space where you can print a full part without hitting the wiper or curing lamp. The gantry can move 360mm, but the first 5mm on each side is reserved for cleaning the nozzles between layers. I’ve tested this dozens of times—printing a test cube at 355mm would leave a tiny edge sliver of support material because the wiper can’t reach that far, so you end up with a failed print. That’s not a bug, that’s MJP’s design working as intended. Our mid-range model, which most aerospace and medical prototypers use, jumps to 500mm x 500mm x 550mm. That’s big enough to print a full-scale prosthetic socket for an adult, or a 1:10 scale drone wing. And our industrial MJP machine, the workhorse for low-volume production, has a usable build volume of 800mm x 600mm x 700mm. That’s space for a full-size bicycle frame prototype—something you can’t pull off with most desktop FDM printers.
But here’s the thing: build volume isn’t one-size-fits-all even for MJP. It depends on what material you’re using. Wait, that sounds counterintuitive, right? But hear me out. We print with three main material types for MJP: rigid photopolymers, flexible elastomers, and high-temperature resins. When you print with flexible elastomers, the support material has to be thicker to hold the part steady during printing. That means the build volume’s height gets cut by about 10mm. Last month, a customer was printing a flexible seal for a HVAC system, and he asked why his 500mm tall seal turned out only 490mm. I explained: his elastomer required a thicker support perimeter, so the machine’s software automatically reduced the usable height to make room. It’s not a flaw in the machine—it’s adaptive. For high-temperature resins, which cure with a stronger UV light, we actually have to leave a 15mm gap at the top of the build volume to prevent light from bleeding over and curing parts that aren’t supposed to be there. That’s why even though the gantry can reach 710mm, the maximum height for high-temp prints is 685mm.
Another factor people ignore: part orientation. If you’re printing a tall, thin part, you can’t just plop it in the middle. You have to leave space around it for the support structures that MJP uses. Those supports aren’t just thin lines—they’re solid wax structures that hold overhangs, like when you print a shelf that sticks out from a wall. A 20mm overhang on a part that’s 300mm long means you need 20mm of support on each side, so your total length used goes from 300mm to 340mm. If you’re printing multiple small parts at once, you can nest them to save space, but the software has to account for the support gaps between parts. I once had a customer who tried to print 20 small phone cases all at once, thinking he could fit them all in the 500mm bed. He only fit 16 because the software required 5mm of space between each case to remove the wax supports without damaging the parts. That’s a huge difference in usable build volume right there.
Now, let’s address a common myth: bigger build volume is always better. Last year, a startup came to me wanting the largest industrial MJP machine, thinking they could print their entire product— a 2-meter long medical device—in one piece. When I showed them the specs, they realized they didn’t need that. A 2-meter part would have required too much material (over $1,200 worth of resin, just for the part, not including support) and would have taken 72 straight hours to print. Instead, we recommended our mid-range machine, and their design team split the part into three sections, each 500mm long, that bonded seamlessly after printing. They saved 60% on material and finished the project in 24 hours total. That’s the tradeoff: build volume isn’t just about size, it’s about matching it to your project. A 3D printer with a 1,000mm build volume sounds impressive, but if you only print small prototypes, you’re wasting thousands of dollars on unused space every year.
So how do you figure out the right MJP build volume for your needs? Let’s walk through it. First, measure the largest dimension of the part you want to print, accounting for any overhangs or supports. If your part is 250mm long, 100mm wide, 150mm tall, a 350x350x400mm entry-level machine is perfect. If you’re printing full-size functional parts, or batches of parts that add up to a large footprint, go for the mid-range 500mm. If you’re printing large prototypes or low-volume production runs, the 800mm industrial model is worth the investment. And don’t forget to account for material-specific adjustments—if you work with flexible or high-temp materials, add 10-15mm to your maximum height to be safe.
Now, as someone who’s been in this industry for years, I’ll also tell you: build volume is only half the equation. The other half is resolution, material compatibility, and post-processing support. We’ve seen machines with huge build volumes that print terrible quality parts, because the nozzle spacing is too wide. Our MJP printers have a 16-micron nozzle resolution, so even at the maximum build volume, your parts come out smooth, no layer lines that require hours of sanding. And when you need to remove the wax supports, our team provides free, step-by-step training on post-processing, so you don’t ruin a $500 part because you pulled too hard.
If you’re still not sure which build volume is right for you, or if you have questions about how the MJP process works for your specific project, I’d be happy to walk through it with you. Whether you’re a small business testing your first prototype, a manufacturer scaling production, or a researcher working on a new medical device, we can help you pick the machine that fits your needs, not just the biggest number.

Don’t guess on build volume—get the right size for your work. Reach out to us today to discuss your 3D printing needs, and we’ll help you find the perfect MJP printer for your projects.
Jewelry 3D Printer References
- ISO/ASTM 52911-2:2019, Additive manufacturing — Requirements for buy-to-fly ratio for feedstock and final parts — Part 2: Polymer.
- Wohlers, T. T. (2023). Wohlers Report 2023: Additive Manufacturing and 3D Printing Global State of the Industry. Wohlers Associates.
- ASTM F2924-14(2021), Standard Specification for Additive Manufacturing Polymeric Material Jetting.
- International Organization for Standardization. (2022). Additive Manufacturing — Terminology for Polymer Material Jetting Processes. ISO 17296-4:2022.
Hangzhou Originator 3D Technology Co., Ltd.
Hangzhou Originator 3D Technology Co., Ltd. is one of the most experienced mjp 3d printer manufacturers and suppliers in China. With abundant experience, we warmly welcome you to wholesale high quality mjp 3d printer made in China here from our factory. Contact us for more details.
Address: Room 403, Building 2, Block B, Heda Incubation Park,No. 452, 6th Avenue, Xiasha, Qiantang District,Hangzhou, Zhejiang, China
E-mail: Sales@originator3d.com
WebSite: https://www.originator3d.com/
