If you’ve ever shopped around for a CNC turning center frame before, you know the big differences between the good stuff and the kind that’ll leave you troubleshooting offsets and part errors after install. As a guy who’s been supplying these frames for almost 12 years, I get asked all the time: “How do I actually measure the machining accuracy of a CNC turning center frame?” It’s not just a numbers game—too many people rely on vague specs from catalogs, which means they end up with a frame that looks fine on paper but won’t hold up to 10-hour production runs. Let me break this down the way I teach my techs when we prep frames to ship. CNC Turning Center Frame

First off, stop confusing “machining accuracy” with just how straight a rail looks. A CNC turning center frame doesn’t just hold the headstock and tailstock; it’s the backbone that absorbs cutting forces, so any distortion there means your spindle won’t rotate true, your linear axes will wander, and you’ll wind up with tapered parts or inconsistent surface finishes. All of that starts with how we measure three core areas: the alignment of the main spindle bore, the linear axis ways, and the flatness of the mounting surfaces for all the critical components.
Let’s start with the spindle bore because that’s the heart of any turning frame. I’ve seen plenty of frames that pass a basic “spin the test indicator around the bore” check, but skip the roundness and concentricity tests. Here’s the actual process we use in our shop. First, we pull a precision mandrel—nothing fancy, just a ground steel rod with a calibrated diameter that fits tight into the spindle bore. We’ll clean the bore super well first, because even a tiny bit of swarf or oil can throw readings off. Once the mandrel is seated, we mount a dial indicator on a magnetic base, clamp it to the lathe bed, and touch the tip to the surface of the mandrel, right at the front of the spindle. Then we slowly turn the spindle by hand, 360 degrees, and note the difference between the high and low readings. That total is the runout at the spindle face. But don’t stop there—move the indicator back, about halfway down the bore, and do the same check. If the runout at the back of the spindle is more than it is at the front, that means the bore is tapered. A tapered spindle bore will cause your bar stock to twist as it feeds, which means your parts won’t hold tolerance for long runs. We spec that max runout at both ends to be less than 0.001 inches for our standard frames—if it’s over that, we don’t ship it, no exceptions.
Next up, the linear ways, which are the rails that the tool slide and tailstock move on. This is where a lot of cheap suppliers cut corners on machining, and that’s why their frames develop “play” after a few months. The ways have to be straight, both along their length and parallel to each other, because if they’re off, your tool won’t move in a perfectly straight line. The tool slide’s Z-axis travel has to align with the spindle centerline, and the X-axis has to be square to that too. How do we measure that? We use a laser interferometer—yeah, it’s not the cheapest tool, but it’s way more accurate than a straightedge for long runs. First, we mount the laser unit to the spindle, then a reflector on the tool slide. We move the slide along the full length of the Z-axis, and the laser logs every tiny deviation from a straight line. I’ll be honest, not every customer needs sub-micron accuracy for a hobby machine, but for production shops running 10,000 parts a month, that 0.0005 inch of deviation over 10 feet can add up to a bad part every 50 pieces. We also check the parallelism of the two ways (the ones for the tool slide and the tailstock) by placing a precision bar of known length between two test indicators, one on each way, then sliding it along. The difference between the two indicators’ readings at every point along the travel tells us how parallel the ways are. If they’re not parallel, the tailstock will bind, and you’ll get distorted parts.
Then there are the mounting surfaces. These are the flat pads where the headstock, the tailstock, and the servo motors bolt down. If these are warped or not flat, even if your ways are perfect, the headstock will lean a little, throwing the spindle centerline out of alignment. How do we check flatness? We use a granite surface plate, a set of precision feeler gauges, and a dial indicator. First, we clean the mounting surface completely—no grease, no leftover machining chips, not even a fingerprint. Then we place the frame’s mounting pad on the surface plate, and set the dial indicator base on the plate itself, so the tip touches the top of the pad. We move the indicator across the entire surface, taking readings every inch or so. Any gap larger than 0.0002 inches between the pad and the feeler gauge means the surface isn’t flat enough. For our frames, all mounting surfaces are milled to a flatness of less than 0.0001 inches per square inch. That might sound overkill, but I’ve seen a customer try to save a few bucks on a frame with a warped headstock mount—they ended up having to re-machine the headstock themselves, which cost them three times what they saved in the first place.
Wait, let’s not forget thermal stability. A lot of guys skip this, but if you’re running a CNC turning center 24/7, heat from the spindle and the servo motors will make the frame expand, and that throws accuracy off over time. We test that by running the spindle at 80% of max RPM for two hours, then taking the same spindle runout and way alignment measurements we did cold, and compare them. A good frame will have a cast iron base with ribbing that disperses heat, so the change in accuracy is less than 0.0003 inches. Cheaper frames use thin steel or cheap cast iron that warps easily—we had a customer test one of our frames against a competitor’s last year, and theirs saw 0.002 inches of shift after two hours, while ours barely moved. That’s the difference between a frame that holds tolerance for a month and one that needs adjustments every week.
Now, let’s talk about common mistakes people make when measuring. First, they don’t account for the weight of the components. The headstock is a big, heavy hunk of metal, right? If you measure the frame empty, then bolt on the headstock, the mounting surface will flex a little. We always measure the frame after it’s assembled with the headstock, tailstock, and linear axes, not just the bare frame. Another mistake is not checking for vibration at high speed. We do a dynamic test where we run the spindle at max RPM with a dummy tool in the holder, and use a vibration meter attached to the frame. If the vibration exceeds 0.1 g, that means the frame is too flexible, and you’ll get chatter marks on your parts. Chatter isn’t just a cosmetic issue—it can wear out your tools twice as fast, which adds more cost.
As a supplier, this is how we ensure every frame we send out meets our specs. We don’t just send a frame and cross our fingers. We do a full accuracy test, log all the readings, and include a test report with every shipment. That report has the spindle runout, way parallelism, flatness of all mounting surfaces, and thermal shift data. A lot of suppliers will give you a vague accuracy number, like “±0.001 inches,” but if you ask for the test report, you can see exactly how we got that number.
If you’re in the market for a CNC turning center frame, don’t just go by price. Ask for the accuracy test data. If a supplier can’t provide that, that’s a red flag. And don’t get stuck on just one measurement—check all the areas I talked about, because accuracy in one place doesn’t mean accuracy everywhere.
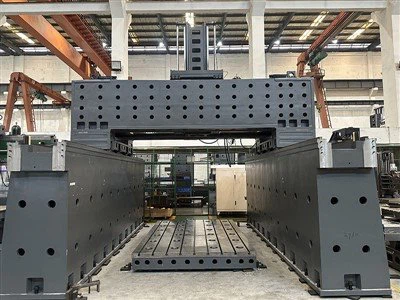
At the end of the day, your frame is the foundation of your machine tool. If it’s not accurate, nothing else will matter. We’ve been doing this for years, and we stand behind every frame we sell. If you’re ready to talk specs, get a test report, or just ask more questions about accuracy checks, feel free to reach out. We’d be happy to walk you through what we do and make sure you get a frame that works for your shop.
T Structure Hmc Machine References
- American Society of Mechanical Engineers (ASME) B5.54-2021, Method for Performance Evaluation of CNC Turning Centers
- Machining Accuracy: Theory and Practice, 3rd Edition, by Yung C. Shin and Steven Y. Liang
- CNC Machine Tool Frame Design and Testing, Society of Manufacturing Engineers (SME)
- Laser Interferometry for Machine Tool Alignment, National Institute of Standards and Technology (NIST) Technical Note 1826
Smartech Machinery & Equipment Co., Ltd.
As one of the most professional cnc turning center frame manufacturers and suppliers in China, we also support customized service. Please rest assured to buy bulk cnc turning center frame made in China here from our factory. Contact us for more details.
Address: Room 2832, Changping Commercial Mansion, Shihua Road, Futian Free Trade Zone, Shenzhen, China
E-mail: smartech@smartechcnc.cn
WebSite: https://www.smartech-cnc.com/
